What are the steps in deep hole drilling process?

The process of professional deep hole drilling can be roughly divided into the following steps:

1. During the process of entering the guide hole, the deep hole drill does not have any support, and the spindle speed needs to be controlled within a certain range. If the speed is too high, the tool will be broken under centrifugal force.

2. The deep hole drill enters the guide hole, and during this process, the deep hole drill has not actually cut yet. However, under the drive of the spindle, the tool will move in the radial direction. Even if the spindle speed is low at this time, the tool will inevitably rub against the guide hole wall, so the tool needs to be fed low during this process. When the deep hole drill moves to a distance of about 1 mm from the bottom of the guide hole with constant processing parameters, the machine tool opens the cutting fluid circulation (providing cooling, lubrication, and chip removal for subsequent processing).

3. The next step in the process, usually to save time and optimize the processing program, is to use deep hole drilling with low feed and low speed processing to 2-3 times the diameter depth, which increases the spindle speed and tool feed without taking any measures. This process has drawbacks, such as φ The performance of tools below 5 is significant, and the sudden change in feed during processing has a significant impact on the cutting edge, which can exceed the bearing capacity of the tool itself, leading to blade breakage. This situation is very dangerous, but if the blade breakage is not replaced in a timely manner, there is a risk of tool breakage.

4. Deep holes are usually connected to other holes. When the tool is processed to the penetration position, the force on the cutting edge of the tool changes sharply, manifested in the cutting edge not cutting at the same time, but first and then, so that the first cutting edge loses support, and the balance of support force on both sides is broken. The tool is affected by the cutting force on the other side, causing the drill bit to shift and deviate too much, which is reflected in the tool and the tool will break; This is reflected in changes in the positional accuracy of the workpiece, and the parallelism of the deep hole will exceed the tolerance. This situation is inevitable in machining. To effectively reduce the problems of tool breakage and poor positioning, the spindle speed and feed should be reduced to 1/3 of the original data at a distance of 5 mm from the through position. This can effectively reduce the force imbalance of the tool during cutting, and the positional accuracy and parallelism are also greatly improved.

5. Tool retraction: Due to the processing characteristics of deep hole drilling and the limitations in parallelism, the tool may experience bending deformation in the hole during retraction. Therefore, rapid retraction cannot be used, but the speed and feed can be faster than the feed. The specific parameters can be determined based on the actual processing conditions.

if you still have question to deep hole drilling, you can contact me sales@btadrilltools.com
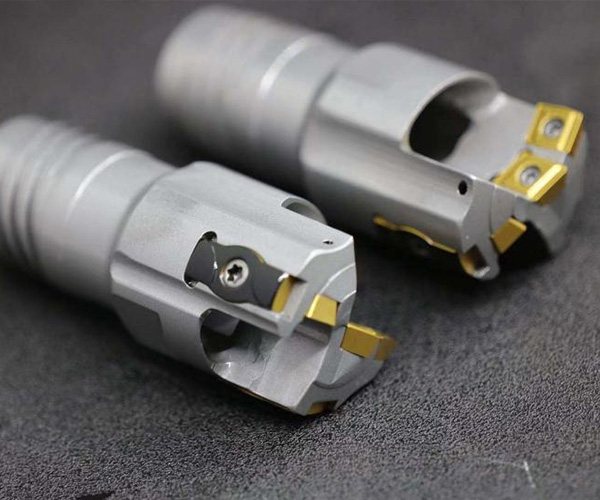
Deep Hole Drilling Machine

Deep Hole Drilling Machine

The deep hole drilling and boring is special equipment for machining deep cylindrical hole of workpieces.It suitable for drilling and boring the cylindrical workpiece.

The machine is controlled by PLC or CNC , the reciprocating movements of guide carriage and feeding carriage are controlled by the servo motor.The drive is made by the racks in the two to ensure long movement feeding transmission accuracy and rigidity requirements. The protection on the two sides of the bed body and the use of the ground oil tank structure improve machine tool environment. The machine can be equipped with two automatic or manual expansion efficient tool,it greatly improves the machining efficiency.

Product Description

model
item
  T2110G、T2110G/1  T2120G、T2120G/1  T2125G、T2125G/1  T2136G、T2136G/1
the range of drilling diameterφ20~60mmφ40~80mmφ40~80mmφ40~80mm
the range of boring diameterφ40~100mmφ40~200mmφ40~250mmφ80~360mm
the height of center400mm400mm400mm500mm
the range of boring depth1000-5000mm1000-10000mm1000-10000mm1000-12000mm
the diameter of chucksφ400mmφ400mmφ400mmφ500mm
workpiece clamped dia. Range of steady restφ50~φ400mmφ50~φ400mm  φ50~φ400mm  φ100~φ500mm
range and kinds of spindle speed70~1200r/min 3 grades 12 kinds70~1200r/min 3 grades 12 kinds70~1200r/min 3 grades 12 kinds50~800r/min 3 grades 12 kinds
the power of main motorN=15kWN=30kWN=30kWN=30kW
range of feeding speed5~2000mm/min ( stepless)5~2000mm/min ( stepless)5~2000mm/min ( stepless)5~2000mm/min ( stepless)
feeding motorN=4.5kWservo motorN=4.5kW servo motorN=4.5kW servo motorN=4.5kW servo motor
guide carriage motorN=6.7kWservo motorN=6.7kW servo motorN=6.7kWservo motorN=6.7kWservo motor
cool pump motor powerN=5.5kW n=1440r/min( two group) N=7.5kW n=960r/minN=5.5kW n=1440r/min
( two group)
N=5.5kW n=1440r/min( four group)N=22kW n=1440r/min( two group)
rated pressure of cooling system2.5Mpa、6.3 Mpa2.5MPa2.5MPa2.5MPa
the flow of cooling system80、180、280L/min100、200、300、 400L/min100、200、300、 400L/min0~800L/min
model
item
T2150T2150Z
the range of drilling diameterφ40-φ100mmφ40-φ120mm
the range of boring diameterφ50-φ500mmφ250-φ500mm    
if need,can reach φ630mm
the range of boring depth2000~12000mm2000~16000mm
workpiece clamped dia. Rangeφ300~φ650mmφ300~φ1000mm
the diameter of headstock spindle hole  φ130mm 
the power of main motorN=30kW,n=960r/minN=55Kw  DC
the taper of spindle boreMetric 140#
range and kinds of spindle speed3.15~315r/min 21 kinds20~200r/min( four grade stepless)
range and kinds of drilling box
speed
  60~1000r/min 12 kinds20~600r/min( three grade stepless)
the power of drilling box motorN=30kW,n=1460r/minN=45kW,frequency motor
range of feeding speed5~1000mm/min ( stepless)5~1000mm/min ( stepless)
range of rapid speed of carriage2000mm/min2000mm/min
the motor of guide carriageN=7.5Kw YASKAWA AC servo motorN=11Kw
feeding motorN=7.5Kw YASKAWA AC servo motorN=11Kw YASKAWA AC servo motor
cool pump motor powerN=11kW n=1440r/min(4组 group)N=22kW n=1440r/min(2组 group)
the rated pressure of cooling system  2.5MPa  2.5MPa;
the flow of cooling system200、400、600、800L/min;0~800L/min;
the main machine precisionIT7-IT9IT7-IT9
the max. weight of workpiece10t20t